Map Failure Modes First to Cut Scale Up Risk in Additive Selection
Map Failure Modes First to Cut Scale Up Risk in Additive Selection ! Additive selection scale-up risk title card Start by matching the dominant formulation failure mode to the additive family responsible for it, then run a short lab feasibility trial alongside a supplier capability check before comm…
Start by matching the dominant formulation failure mode to the additive family responsible for it, then run a short lab feasibility trial alongside a supplier capability check before committing to a line item. Selection decisions should be judged on compatibility, cost-in-use, compliance exposure, and scale-up risk, not unit price alone. The immediate next step is a targeted screening: one additive family, one failure mode, one qualified supplier willing to document the result.
TL;DR:
- Additive selection should begin with identifying the primary failure mode and matching it to the correct additive family for targeted testing, avoiding mixed trials that obscure results.
- Evaluation matrices must weight factors such as performance, compatibility, process stability, and supply security, with cost-in-use scored last to prevent price bias.
- Compatibility testing must replicate actual plant conditions, including shear, temperature, and addition sequence, to ensure lab results predict real-world behavior.
- Reliable supplier documentation and in-house formulation capabilities significantly reduce risks related to quality, scale-up, and regulatory compliance during formulation development.
- Conducting a sequence of five key tests—including pilot runs, feed-sequence trials, and stability checks—ensures additive performance before full-scale production, guided by clear ownership and documentation.
Additive selection support starts with correct diagnosis. Coating, adhesive, ink, plastics, and composites formulators lose weeks chasing the wrong additive family because they shortlisted by product name instead of by the defect they were actually seeing on the line. Longchang Chemical's guidance makes the same point for coating and ink systems: choose additives by the formulation problem you need to solve, not by brand recognition.
The mapping is more consistent across industries than most technical directors expect:
- Flow and leveling defects (orange peel, brush marks, uneven film buildup) point to leveling agents first.
- Pigment settling, flooding, or color drift point to dispersants.
- Poor substrate wetting or crawling point to wetting agents.
- Craters, fisheyes, or surface contamination point to specialty surface additives.
- Foam entrapment during mixing or application points to defoamers.
Lab signs and plant signs often disagree, which is exactly where the diagnosis goes wrong. A batch that looks stable in a quart can under lab shear may foam heavily under high-speed plant dispersion, or a dispersant that resolves settling in storage may still flood under spray application. Start screening with a single additive family tied to the single dominant failure mode. Mixing two candidate families in the same trial muddies the signal and makes it impossible to tell which change fixed, or caused, the outcome. Keep the first round clean, then widen the shortlist only after the primary failure mode is resolved.
What Should a Weighted Additive Scorecard Include?
A defensible shortlist needs a scoring method, not a gut call on price per kilogram. A practical evaluation matrix scores candidates across five factors, weighted by application class rather than treated as equal by default.
- Performance effectiveness — does the additive resolve the target failure mode at the tested dosage without introducing a secondary defect?
- Compatibility — does it interact cleanly with resins, pigments, and other additives already in the system?
- Compliance and EHS exposure — does it carry labeling, VOC, or handling requirements that complicate downstream use?
- Process stability at scale — does performance hold under plant shear, temperature, and residence time, or only under lab conditions?
- Cost-in-use and supply security — does the true operating cost, not the quoted unit price, justify the switch, and can the supplier maintain volume reliably?
A coatings formulator chasing appearance defects might weight performance and process stability at 30 percent each, with compliance and cost-in-use at 20 percent each and compatibility filling the remainder. An adhesives producer working near regulatory limits might invert that, weighting compliance and compatibility higher.
Lab measurements convert directly into score inputs: dosage required to hit target viscosity, percent viscosity drift after accelerated aging, and appearance rating after shear cycling. Score two generic dispersant candidates side by side. Candidate A hits target viscosity at a lower dosage but shows 15 percent viscosity drift after two weeks of storage. Candidate B needs a higher dosage but holds flat. Candidate B usually wins the pilot slot once cost-in-use accounts for the rework risk behind Candidate A's instability.
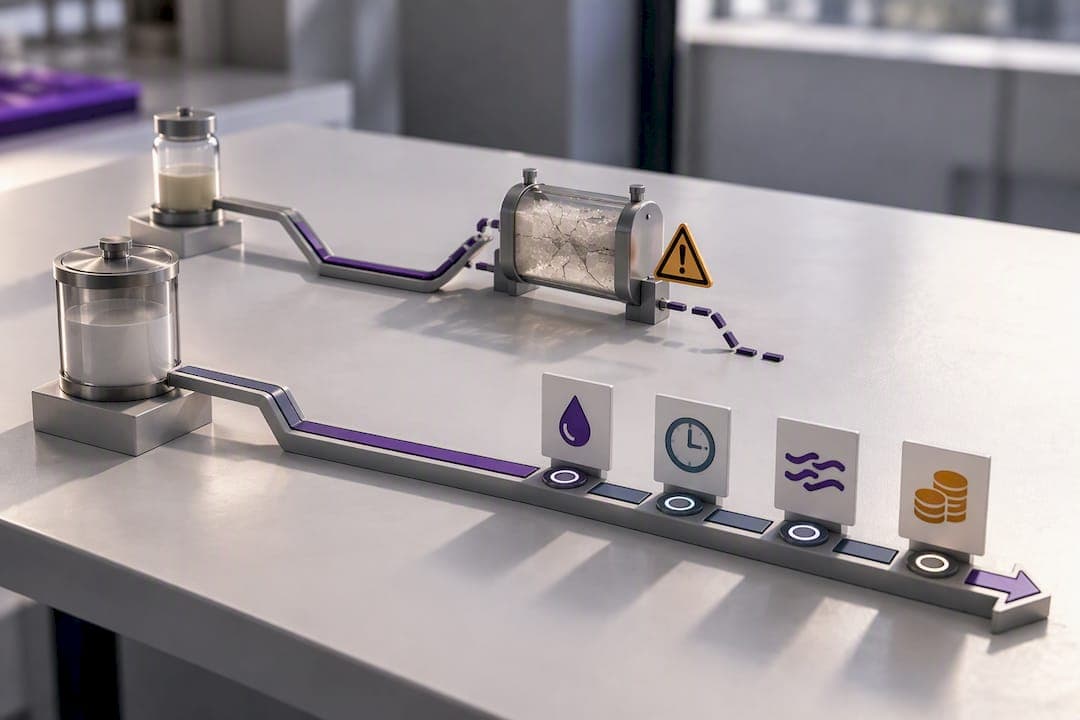
Pro Tip: Weight cost-in-use last in your scoring pass, not first. Teams that score price before performance tend to anchor on the cheapest option and then rationalize its compatibility gaps instead of catching them.
How Should Compatibility Testing Mirror Production Conditions?
Lab screening only earns its keep when it replicates plant reality, not bench convenience. Evaluation guidance for chemical formulations recommends designing short trials that match actual mixing speeds, temperatures, and residence times, because additives that behave predictably at low shear frequently fail once they hit high-speed dispersion equipment.
The minimum test set for additive selection support should cover:
- Compatibility with every other raw material already in the formulation, not just the resin or base polymer.
- Thermal and storage stability across the expected shelf-life window.
- Shear and mixing tolerance at plant-representative speeds.
- Feed-sequence trials, since addition order changes outcomes more often than formulators expect.
- Packaging stability, particularly for moisture-sensitive or reactive systems.
Ask any candidate supplier for a feasibility study, a starting formulation, and analytical data covering FTIR, GC/MS, viscosity, and stability results. Suppliers with in-house formulation labs routinely run this compatibility work under NDA, which shortens the internal screening cycle considerably. Put an NDA in place before sharing proprietary base formulations, and confirm the supplier's data-handling terms before any sample exchange begins.
What Supplier Capabilities and Documents Reduce Qualification Risk?
Selection support is only as strong as the documentation behind it. Procurement should require current SDS sheets, batch COAs, impurity and spec limits, shelf-life data, and origin or supply-continuity statements before a supplier moves past initial screening. Reliable suppliers provide this documentation as a matter of course, and treating it as an acceptance criterion, not a courtesy, catches problems before they reach the plant floor.
Beyond paperwork, the capabilities that separate a transactional vendor from a genuine formulation partner include:
- An in-house formulation lab with feasibility-study capacity.
- Analytical methods on hand, including FTIR, GC/MS, Karl Fischer, and viscosity testing, so batch-to-batch consistency can be verified rather than assumed.
- Documented scale-up experience moving from small batches to full production runs.
- Packaging, logistics, and contingency planning that account for feedstock volatility.
Each capability maps to a specific risk. Analytical rigor reduces quality risk. Scale-up history reduces timeline risk. Documented supply contingency reduces the regulatory and delivery risk that shows up only after a formulation is already committed to a production schedule.
Which Five Procurement Tests Prevent Scale-Up Failures?
Five checks, run in sequence, catch most of the failures that surface after commercial commitment: a small-batch pilot run, a feed-sequence tolerance test, a full-process residence-time run, a packaging and stability trial, and documentation and traceability verification. Contractual milestones built around these tests tied to yield, appearance, and process-stability acceptance criteria keep approval delays from stalling a launch.
- Small-batch pilot run against target yield and appearance specs.
- Feed-sequence tolerance test to confirm addition order doesn't shift outcomes.
- Full-process residence-time run matching actual plant cycle times.
- Packaging and shelf-life stability trial under real storage conditions.
- Documentation and traceability check against the supplier's SDS and COA claims.
Lead times shrink when suppliers offer prioritized sample kits, overlap batches during transition, and framework agreements that lock in safety stock. Astra-chemical structures its formulation support around exactly these tests.
Pro Tip: Ask for overlap batches, not a hard cutover. Running the incumbent and candidate additive side by side for one production cycle catches feed-sequence problems that a single-shot pilot run will miss entirely.
Why Cross-Functional Ownership Decides Whether Additive Trials Succeed
Most trial failures trace back to unclear ownership, not bad chemistry. Procurement should own supplier terms and documentation, R&D should own feasibility and compatibility data, and production should own scale-up acceptance criteria, with a written RACI before any additive enters trial. Engaging supplier formulation labs under NDA consistently shortens the feasibility timeline, which is reason enough to make that step routine rather than exceptional.
— Astra R&D Team
Get Formulation Lab Support for Your Next Additive Trial
Most additive suppliers hand you a spec sheet and a sample; getting an actual feasibility study back within your project timeline is the harder part. Astra-chemical runs its own in-house formulation lab, so a compatibility trial for dispersants, silicone or non-silicone defoamers, and rheology modifiers starts with real analytical data instead of a generic recommendation.
That lab-backed qualification is how Astra-chemical keeps total cost-in-use below premium-brand pricing without cutting corners on batch consistency or documentation. If you're already comparing suppliers for an active formulation problem, browse the full additive catalog to identify the family that matches your failure mode, then request a sample kit or a technical consultation to get a feasibility run scheduled against your actual production conditions.
Sources
For deeper grounding on the mechanics covered above, see the additive selection checklist, the evaluation matrix framework, and supplier leverage guidance referenced throughout this checklist.
- CHLUMICRYL® Coating and Ink Additives: How to Choose Additives for Flow, Wetting, Dispersion, and Surface Performance - Longchang Chemical
- How to Evaluate a Chemical Formulation for Additives
FAQ
What Is Additive Selection Support, Exactly?
It's the technical and procurement guidance that helps formulators pick the right additive family, dosage, and grade for a specific defect, then verifies that choice through lab and pilot testing. It combines formulation diagnostics with supplier documentation checks and scale-up trials rather than relying on a spec sheet alone.
How Does Additive Selection Support Work in Practice?
It starts by mapping the observed defect (foaming, poor flow, pigment settling) to the additive family most likely to resolve it, then runs a focused lab screening against that single family. Supplier capability, documentation, and cost-in-use get scored alongside performance before any pilot batch is approved.
What's the Fastest Way to Shorten Additive Lead Times?
Ask suppliers for prioritized sample kits and overlap batches during any transition, and lock in framework agreements that guarantee safety stock. Suppliers with in-house formulation labs can also turn around feasibility data faster than vendors without dedicated technical support.
What Documentation Should a Supplier Provide Before Qualification?
Current SDS, a batch-specific COA, impurity and spec limits, shelf-life data, and an origin or supply-continuity statement. Sourcing checklists for coating and adhesive chemicals treat this documentation as a formal acceptance gate, not an optional extra.
Does Astra-chemical Offer Sample Kits for Trial Runs?
Yes, Astra-chemical supports feasibility work through its product lines, including ASTRA DISP® dispersants and ASTRA DF® defoamers, with sample requests and technical consultations available through its product catalog. Pricing for specific grades is available on request through that page.
Recommended
Testing additives for this application?
Send us your current formulation challenge and our technical team will recommend an ASTRA product package for lab screening.