Ink Viscosity Control: Measurement, Adjustment, Formulation
Ink Viscosity Control: Measurement, Adjustment, Formulation ! Operator measuring printing ink with an efflux cup Ink viscosity control is the practice of holding an ink's resistance to flow inside a predetermined range, by monitoring it continuously and correcting it to specified limits, so that ink…
Ink viscosity control is the practice of holding an ink's resistance to flow inside a predetermined range, by monitoring it continuously and correcting it to specified limits, so that ink transfer, color strength and drying remain constant from the first impression to the last. Two disciplines share the task: the press room, where solvent, water or fresh ink is metered in to offset drift, and the formulation laboratory, where pigment dispersion, foam behavior and rheology are engineered so that the ink drifts less to begin with. This guide covers both, for flexographic, gravure and corrugated printing.
TL;DR
- Viscosity governs ink transfer, color density, drying and waste, so it is specified, measured and corrected during every run, not only at make-ready.
- Temperature, solvent evaporation, shear history and storage conditions are the main causes of drift; automatic control compensates with frequent small corrections rather than occasional large ones.
- The correct target comes from the ink manufacturer and depends on ink type, anilox or cylinder specification, press speed, substrate and temperature.
- Formulation reduces the burden on the press: well-dispersed pigment, controlled foam and a deliberately designed rheological profile make viscosity easier to hold.
Viscosity is the ink's resistance to flow. In flexographic, gravure and corrugated printing the term covers three linked activities: measuring the ink at a defined condition, comparing the reading with the specified window, and adjusting the ink when the reading leaves it. Adjustment typically means adding solvent or water to thin an ink that has thickened, or adding virgin ink to restore solids when the ink has been over-diluted.
The corrugated-printing guidance published by a viscometer manufacturer states that operators should maintain viscosity consistent with acceptable printability and, when required, add virgin ink, verify that the ink suits the substrate, confirm the formulation and check or adjust pH to job specifications. Viscosity is therefore one of several linked ink parameters, not a standalone number.
Inline instruments add one further refinement. Real-time monitoring measures viscosity from a baseline rather than relying only on absolute values, which makes the trend visible before it becomes a defect.
Why viscosity drives color, transfer and waste
Viscosity is a proxy for the quantity that gives an ink its color. It is an indicator of the ink's percent solids, and the pigment load sits within those solids. When viscosity wanders, pigment concentration wanders with it.
The consequences are measurable:
- Color variation. A gravure press trial reported in a TAGA paper found significantly greater color variation under manual viscosity control than with automatic control of solvent addition. The same study describes how viscosity affects ink transfer, tone gain, color gamut and printed-image quality.
- Over-dilution. Excessive dilution lowers pigment concentration and can weaken color, according to the same TAGA study, which is why solvent is added in measured increments.
- Waste and cost. Poorly adjusted viscosity can lead to substandard print quality, excessive ink consumption and unnecessary costs, while tight control can reduce setup times and scrap.
- Corrugated defects. A flexographic and corrugated viscometer supplier identifies poor viscosity control as a contributor to streaking, halos, smudging, fisheyes and off-colors, together with higher ink usage and waste.
Flexography adds its own sensitivity. Fast-drying inks and soft plates across packaging and other substrates mean that, without stable viscosity, images and messaging may print inconsistently and runs may be rejected.
What makes viscosity drift
Viscosity is not a fixed property of an ink. It changes with temperature, shear rate, flow conditions and pressure. On a running press, four mechanisms dominate.
Temperature
Warmer ink becomes less viscous and colder ink more viscous. A technical article from an ink manufacturer notes that these changes can restrict ink delivery and cause density fluctuation or starvation, while other conditions contribute to dripping, misting, spitting, buildup or setoff. Temperature fluctuations can have a drastic effect on viscosity, which is why heated or chilled ink circuits and temperature-compensated readings are common in automated systems.
Solvent or water evaporation
The TAGA gravure study explains that evaporation during a run changes ink concentration, so solvent addition is needed to maintain operating conditions. The ink in the fountain or chamber therefore grows more concentrated the longer it runs, unless it is replenished.
Press-side dwell time
Viscosity and pH can change while ink sits press-side for hours or days because of environmental conditions. A label printer's measurement guide recommends that printers record and adjust them within established tolerances, alongside density, dryer temperature, anilox specifications and other press conditions.
Storage
Storage matters before the ink reaches the press. For plastisol, one ink supplier recommends sealed containers and storage between 65°F and 90°F (18°C and 32°C), and warns that heat, cold floors, sunlight and partial curing can alter viscosity and printability. Water- and solvent-based inks have their own storage limits, which the technical data sheet of each product specifies.
Measuring viscosity: instruments, units and standards
A reading is only useful when the method is repeatable. Inline and laboratory work use several instrument families, each reporting a slightly different quantity.
| Instrument type | What it reports | Typical use |
|---|---|---|
| Rotary viscometer | Dynamic viscosity (Pa·s) | Laboratory and quality control |
| Efflux cup | Flow time in seconds | Press-side manual checks |
| Tuning-fork sensor | Dynamic viscosity and specific density | Inline monitoring |
| Acoustic-wave sensor | Product of dynamic viscosity and density | Inline monitoring |
| Falling-rod viscometer | Apparent viscosity and non-Newtonian behavior of paste inks | Production control, supplier-purchaser acceptance |
The instrument list and the unit conventions (dynamic viscosity in Pa·s, kinematic viscosity in stokes or m²/s, efflux-cup seconds) follow an academic evaluation of inline sensors for gravure, which also notes that tuning-fork sensors can calculate dynamic viscosity and specific density while acoustic-wave sensors measure the product of dynamic viscosity and density. That distinction matters when a reading from one device is compared against a specification written for another.
For paste inks, ASTM D4040-10(2019) covers determination of apparent viscosity and non-Newtonian behavior with a falling-rod viscometer and is useful for production control and supplier-purchaser acceptance.
Shear history also affects the number obtained. A National Bureau of Standards report found that reproducible ink-viscosity measurements require control of the measurement procedure and shear history, and that a brief rotary pretreatment at a sufficiently high shear rate can reduce unstable normal forces and yield stable values. Practically, two laboratories reading the same thixotropic ink can disagree if one stirs the sample and the other does not.
Manual versus automatic control
Efflux cups remain widespread because they are inexpensive and quick, but they depend on the operator's timing, cup condition and sampling interval. The TAGA researchers' view is that automatic control outperforms manual cup measurements because frequent small corrections can compensate for evaporation, whereas operator and flow-cup errors create larger viscosity swings and corresponding color variation.
In gravure, accurate, repeatable viscometers with automatic control can hold viscosity within narrow limits and help ensure consistent color quality over long runs.
On flexographic lines, integrated systems exist as well. One anilox and ink-management supplier describes a unit that measures viscosity with a vibration sensor and controls viscosity and temperature of water- and solvent-based inks within the ink distribution system, and states that such systems reduce maintenance and cleaning time.
A workable control routine, whether manual or automated, follows the same sequence:
- Condition the ink and record temperature before the first reading.
- Measure at the start of the run and compare with the specified window.
- Add solvent, water or virgin ink in small increments, allowing for mixing time.
- Re-measure at fixed intervals, or continuously with an inline sensor.
- Log viscosity next to density, pH and temperature so that drift can be traced to a cause.
Choosing the right target
The target is not a universal number. Printers should use the viscosity advised by the ink manufacturer and monitor it at the start and throughout the run within agreed tolerances, since the right value depends on ink type, anilox specification, press speed, substrate and temperature.
The measurement condition deserves equal attention. A technical white paper on ink analysis advises that values should be measured under conditions that simulate those at the print head. Modern printers can apply shear rates as high as 10^5 to 10^6 s^-1, and inks may need high low-shear viscosity for stability and lower high-shear viscosity for printing. The same document makes the point that no universal ink formulation exists: an ink needs a rheological profile that balances storage stability with performance during printing.
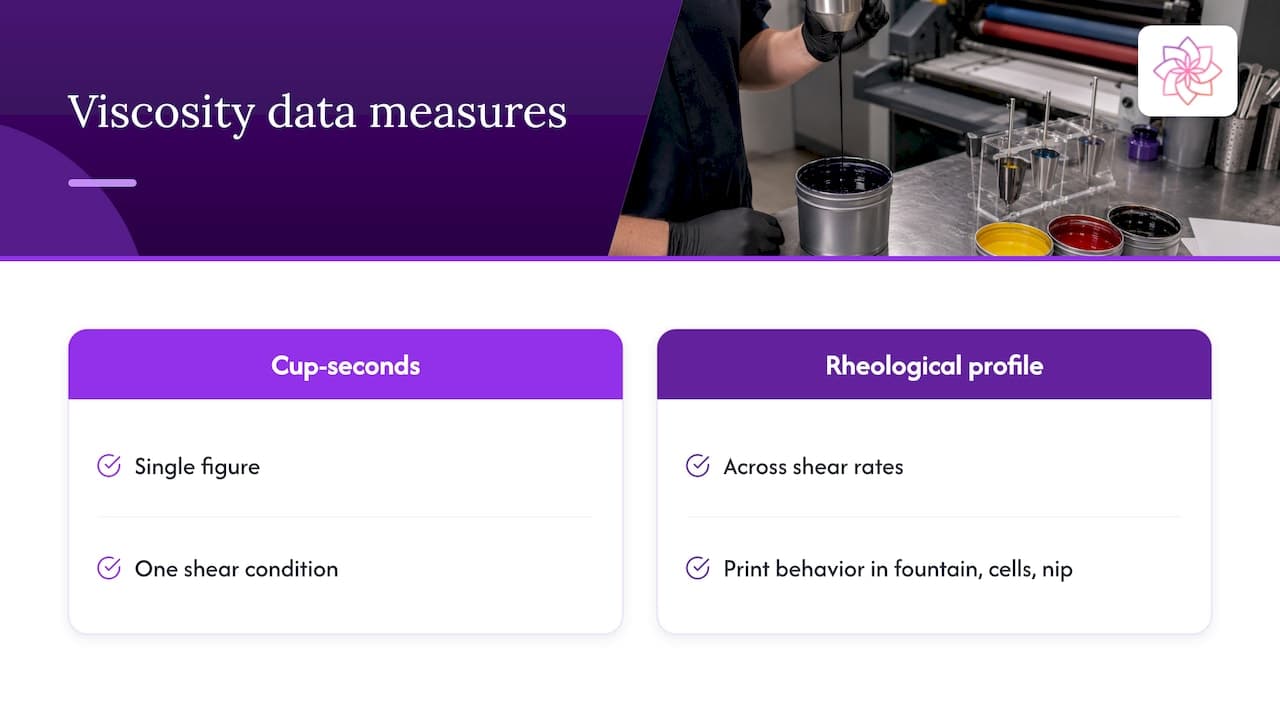
This is the key to reading a technical data sheet correctly. A single cup-seconds figure describes the ink at one shear condition. The rheological profile across shear rates describes how the ink will behave in the fountain, the anilox cells or gravure cells, and at the nip.
Formulation levers that make viscosity easier to hold
Press-side correction treats the symptom. Formulation addresses the cause by narrowing how far viscosity can move. Four levers matter to ink manufacturers.
Pigment dispersion
Poorly stabilized pigment flocculates, and flocculation raises low-shear viscosity and weakens color development. Wetting and dispersing additives adsorb on the pigment surface and stabilize it against re-agglomeration, which is intended to keep the ink's rheology consistent through storage and through the shear cycles of a run. Within the ASTRA line, ASTRA DISP® is the dispersant range for pigmented formulations.
Pigment and filler selection
The pigment itself contributes. In white inks, titanium dioxide grade selection changes viscosity because surface treatment and oil absorption differ between grades. A titanium dioxide producer's ink brochure explains that its alumina/silica-treated grade is recommended for matte flexographic inks and that combining two grades lets formulators optimize opacity and ink viscosity. Pigment choice and dispersant choice should therefore be qualified together.
Foam control
Pumped, circulated and doctor-bladed inks entrain air. Foam distorts the apparent viscosity reading, since entrained air alters the response of inline sensors and cups, and it produces pinholes and uneven laydown on the substrate. Defoamers are selected by chemistry: silicone-based types act strongly at low dosage but require compatibility testing against the risk of surface defects, while non-silicone types suit systems in which silicone is unwelcome. The ASTRA range covers both: ASTRA DF® and ASTRA DF NS® for silicone and non-silicone defoaming respectively.
Rheology modification
A rheology modifier builds the profile described above: sufficient structure at rest to prevent pigment settling, and shear-thinning response under the high shear of printing. The ASTRA REO® line is designed for this purpose. Dosage is determined experimentally, because the effect depends on the resin, solvent or water system, and pigment loading. Readers who work across coatings and inks will find related dosage and selection logic in the guide to reactive diluents and functional additives, and further technical material in the ASTRA CHEMICAL technical blog.
Diagnosing viscosity-related defects
The table below links common press symptoms to viscosity-related causes and a first check. It is a starting point for investigation, not a replacement for ink supplier guidance.
| Symptom | Viscosity-related cause | First check |
|---|---|---|
| Color drifts stronger over the run | Evaporation concentrating the ink | Measurement interval and solvent or water addition rate |
| Color weak after correction | Over-dilution lowering pigment concentration | Add virgin ink to restore solids |
| Density fluctuation or starvation | Cold, thickened ink restricting delivery | Ink temperature at the fountain or chamber |
| Streaking, halos, smudging | Viscosity outside the window, contamination | Reading against specification, filtration |
| Pinholes, uneven laydown | Entrained air or foam | Circulation, pump return geometry, defoamer |
| Viscosity reading unstable | Shear history or sensor fouling | Sample conditioning and sensor cleaning |
The temperature symptoms follow the manufacturer's account cited earlier, and the streaking and smudging entries follow the corrugated analysis from the viscometer supplier; the remaining entries reflect standard process reasoning and should be confirmed against the technical data sheet of the ink in use.
Perspective: viscosity stability starts in the formulation
Our experience supporting coatings, adhesives and ink manufacturers is that viscosity problems reported on the press are frequently formulation problems expressed late. When pigment is only marginally stabilized, or foam is controlled only by a generic additive, the press operator inherits a system that drifts, and no viscometer can fix a dispersion that is re-agglomerating.
For that reason we approach ink viscosity as a joint specification of dispersant, defoamer and rheology modifier, each qualified against the actual resin system, pigment and process. ASTRA DISP®, ASTRA DF®, ASTRA DF NS® and ASTRA REO® are designed to be evaluated together in laboratory-backed qualification, with dosage support aimed at the lowest total cost-in-use rather than the lowest price per kilogram.
Batch consistency matters as much as the additive chemistry. A process control loop tuned to one lot of additive performs predictably only if the next lot behaves the same, and our documentation and technical support are organized around that requirement.
Astra R&D Team
Qualifying additives for an ink system
A structured qualification limits the time spent on trial and error. The sequence below suits most ink systems.
- Define the target: press type, ink family (solvent, water, energy-curable), substrate, and the viscosity window from the ink specification.
- Establish a baseline: measure the unmodified ink at the shear conditions that matter, and record temperature.
- Evaluate dispersant dosage by ladder study, monitoring viscosity, color strength and stability after heat aging.
- Add defoamer at the lowest effective level and check for surface defects and recoat behavior.
- Adjust rheology to restore structure at rest and shear-thinning under printing.
- Validate on press, logging viscosity, density, pH and temperature against the baseline.
Repeating the same measurement method at every step matters more than the choice of instrument, given the sensitivity to shear history noted earlier.
ASTRA additives for ink formulators
ASTRA CHEMICAL manufactures dispersants, silicone and non-silicone defoamers, rheology modifiers and functional additives for coatings, adhesives, inks, plastics and composites, with technical consultation and sample requests available to industrial manufacturers. Formulators who are evaluating a viscosity problem can review the full ASTRA product range and request laboratory samples for qualification.
The product pages list the chemistry of each line, and technical support assists with dosage and compatibility planning for the specific ink system.
FAQ
How often should ink viscosity be measured during a run?
The interval is set by the ink supplier and the press, but the principle is consistent: measure at the start and throughout the run within agreed tolerances. Fast-evaporating systems justify shorter intervals or continuous inline measurement, because evaporation steadily concentrates the ink during the run.
Is an efflux cup good enough, or is inline measurement necessary?
An efflux cup can hold an acceptable window on stable, short jobs. For long runs and tight color tolerances, automatic control is preferred in the TAGA research, since frequent small corrections avoid the larger swings that operator and flow-cup errors produce.
Can additives lower ink viscosity without diluting the ink?
In many systems, yes. Dispersants can reduce the viscosity contributed by poorly stabilized pigment, which allows the ink to retain pigment concentration instead of being thinned with solvent. The effect depends on the resin and pigment system, so dosage should be established by laboratory testing.
Why does the same ink read differently in two laboratories?
The cause is usually method rather than ink. Instrument type, shear rate, temperature and sample pretreatment all change the reported value, and a National Bureau of Standards report found that controlling the procedure and shear history is necessary for reproducible results.
What viscosity should a given ink run at?
The value stated by the ink manufacturer for that ink, anilox or cylinder, speed, substrate and temperature. Generic figures are unreliable because no universal ink formulation exists.
Sources
- Optimizing flexographic, gravure and corrugated printing through inline process monitoring
- Automatic Viscosity Control in Gravure Printing (TAGA)
- Ink-viscosity optimization and automation systems for gravure printing and coating, Part 1
- Why Viscosity Control Matters in Flexographic Printing
- Corrugated eGuide
- How Temperature Affects Ink Performance
- Storing Plastisol Ink Correctly
- Label Printing Essentials: Measurements and Setup
- Evaluation of sensors for inline viscosity measurement in gravure printing
- ASTM D4040-10(2019) Rheological Properties of Paste Printing Inks
- Relationships between mechanical properties and performance, NBSIR 84-2901
- Anilox Ink Management Systems
- The Correct Ink Viscosity is Vital for High-Quality Print
- Analytical strategies for ink formulation
- KRONOS Titanium Dioxide for inks
Testing additives for this application?
Send us your current formulation challenge and our technical team will recommend an ASTRA product package for lab screening.